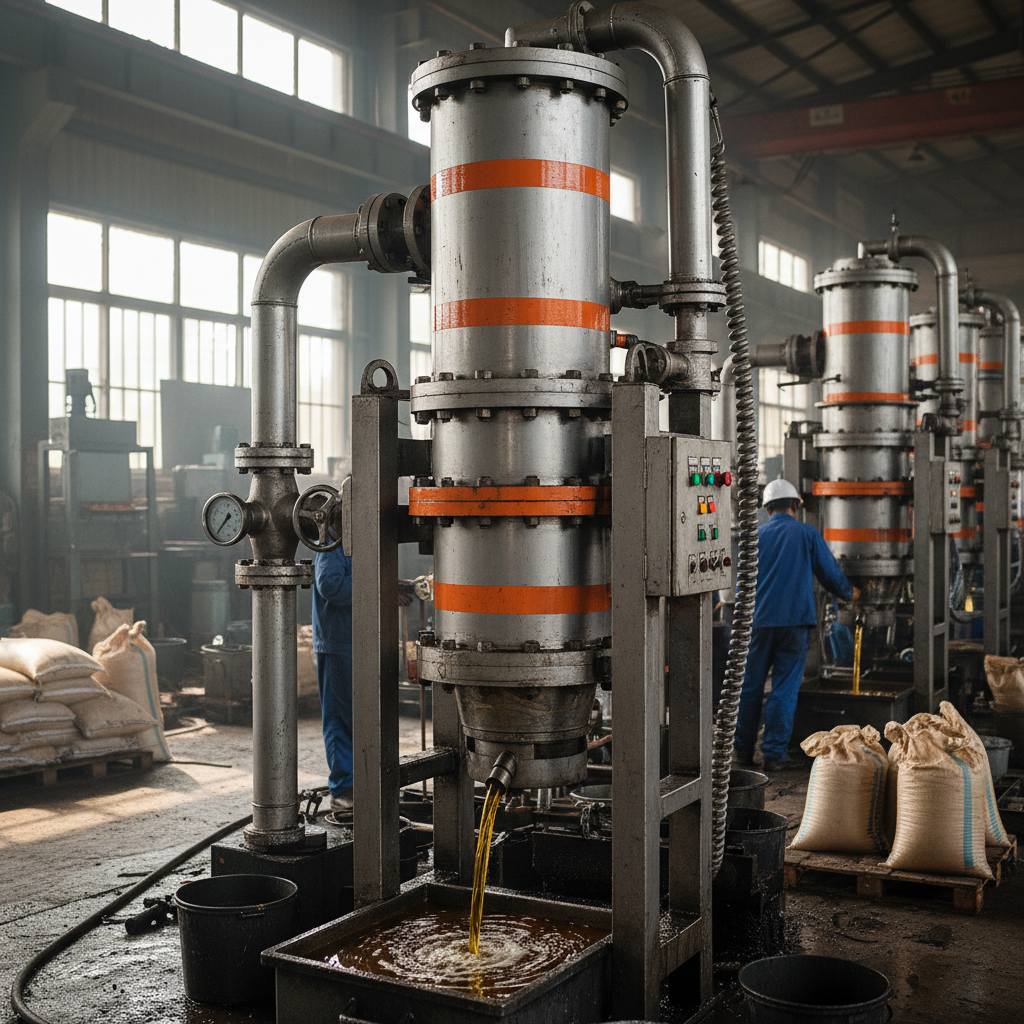
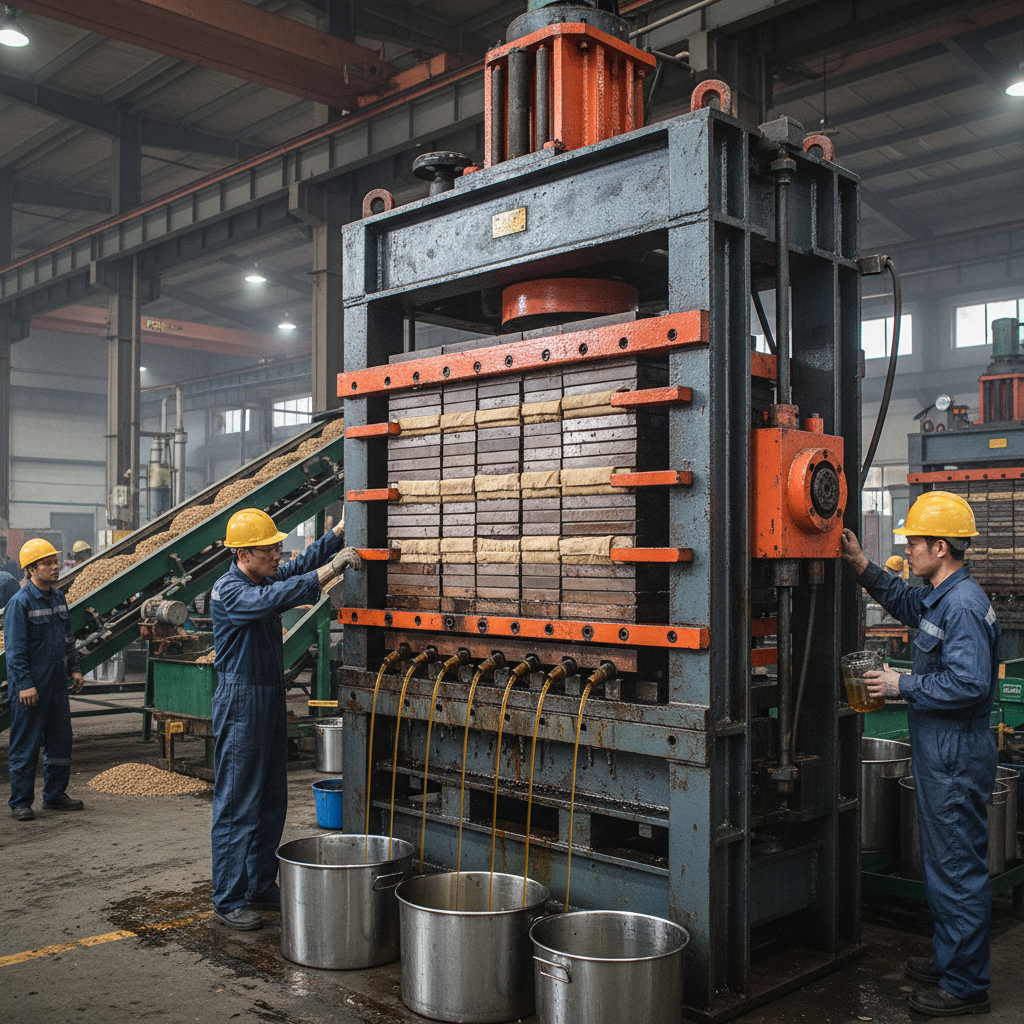
In the global edible oil industry, achieving high purity and efficiency is paramount to meeting food safety standards and consumer demands. The use of a high-performance centrifuge separator is essential for removing impurities, gums, and phospholipids from crude oils, ensuring that the final product is clear, stable, and free from contaminants. By leveraging centrifugal force, these machines accelerate the separation process far beyond what gravity alone could achieve.
Modern oil refining processes face significant challenges, including the need to handle various oil characteristics—from thick palm oil to light sunflower oil—while maintaining maximum production capacity. Inefficient separation can lead to product waste, increased chemical usage, and higher operational costs. The industry requires robust, automated solutions that can operate continuously without compromising the quality of the refined oil.
The centrifuge separator serves as a critical technological hub in this process, offering a sophisticated method for degumming, desoaping, and water washing. By integrating advanced PLC controls and stainless steel construction, these separators ensure that vegetable and animal oils are processed with surgical precision, maximizing yield and ensuring adherence to strict international hygiene standards.
Technical Architecture of Disk Separators
The disk centrifuge separator is engineered to provide personalized solutions tailored to the specific characteristics of various oils. By utilizing a stack of conical disks, the machine increases the effective settling area, allowing for the rapid separation of light and heavy phases. This architecture is particularly effective for vegetable oils such as rapeseed, corn, soybean, and rice bran oil, as well as animal fats like fish oil.
To ensure the highest purity, all components that come into contact with the materials are crafted from high-grade stainless steel. This design choice effectively minimizes chemical reactions between the oil and the machine surfaces, preserving the natural properties of the oil and preventing contamination. The result is a stable, hermetic system that operates at high speeds to maximize production capacity.
Industrial Relevance and Global Application
In the global agricultural processing landscape, the demand for refined edible oils is surging, driven by population growth and shifting dietary habits. A reliable centrifuge separator is no longer an optional luxury but a core requirement for any plant aiming to meet ISO and food-grade certifications. From large-scale refineries in Southeast Asia processing palm oil to boutique olive oil presses in Europe, these machines are the heartbeat of the refining line.
Beyond edible oils, the versatility of this technology extends into the chemical, pharmaceutical, and light industrial sectors. The ability to separate liquids of different specific gravities or remove solids from a suspension liquid makes the DHZ and HPDF series indispensable. Whether it is purifying medicine or processing chemical additives, the precision of centrifugal separation ensures product consistency and safety.
The integration of these machines into continuous refining processes—specifically for degumming and desoaping—has revolutionized the industry. By reducing the reliance on manual intervention and optimizing the water washing phase, producers can significantly lower their environmental footprint while increasing their output, aligning with global sustainability goals.
Core Components for High-Efficiency Separation
The efficiency of a centrifuge separator is largely dependent on its drive system and material handling. The use of a hydraulic coupler combined with helical step-up gears ensures that power is transmitted via liquid, allowing the machine to ramp up speed steadily. This mechanism not only protects the motor from sudden shocks but also provides built-in overload protection.
Automation is handled through a combination of computer controls and PLC systems, which manage the residue-extraction of the slide piston. This highly automated approach allows the centrifuge separator to adapt to changes in the process in real-time, greatly reducing the labor burden on operators and minimizing human error during the discharge cycle.
Finally, the output system utilizes two centripetal pumps of different sizes to efficiently discharge the light and heavy phase materials. Because the machine is fed from the top, it requires very low inlet pressure, which simplifies the plumbing requirements and reduces the energy consumption of the feed pumps, making the overall operation more cost-effective.
Performance Analysis Across Different Models
Selecting the right model of a centrifuge separator depends heavily on the required throughput and the nature of the oil being processed. For instance, the DHZ series offers a range of capacities from 1,200 to 10,000 L/H, making them ideal for medium-sized refineries. In contrast, the HPDF series can handle capacities up to 18,000 L/H, catering to large-scale industrial operations.
The performance varies not only in capacity but also in power consumption and physical footprint. A smaller unit like the HPDF 360 is designed for space-efficiency and lower energy use, while the HPDF 550 is a powerhouse designed for maximum stability under heavy loads. The following chart illustrates the relative performance ratings across different configuration types.
Centrifuge Separator Performance Comparison
Operational Advantages in Oil Refining
One of the primary advantages of using a modern centrifuge separator is the ability to achieve a high degree of automation. By utilizing PLC-controlled discharge, the machine can clear accumulated solids without stopping the flow of oil, ensuring a continuous production cycle. This removes the bottleneck often found in traditional batch-processing methods.
Furthermore, the stability provided by the helical step-up gears and hydraulic coupling reduces mechanical wear and tear. This leads to longer intervals between maintenance cycles and a lower total cost of ownership. When combined with the corrosion-resistant stainless steel build, these machines provide a reliable, long-term solution for high-volume refining environments.
Overcoming Common Refining Challenges
Many refineries struggle with the variability of crude oil quality, which can fluctuate based on the harvest or source. A flexible centrifuge separator solves this by offering adjustable parameters through the PLC system, allowing operators to tune the separation speed and discharge frequency to match the specific impurities of the current batch.
Another common challenge is the high cost of labor and the risk of human error during the residue extraction phase. By automating the slide piston movement, the risk of operational mistakes is virtually eliminated. This not only ensures a safer working environment but also guarantees that the oil is consistently processed to the same high standard.
Finally, the issue of inlet pressure is often a hurdle in plant layout. Because the DHZ and HPDF models are fed from the top, they operate with very low inlet pressure requirements. This allows plants to optimize their piping and pump configurations, reducing the overall energy load and simplifying the installation process in existing facilities.
Technical Specifications and Model Selection
Choosing the correct centrifuge separator requires a careful analysis of your production volume and the specific gravity of the materials being separated. For those operating at a smaller scale, the HPDF 360 or DHZ 360 provides an excellent entry point with capacities around 1,200-2,500 L/H. These models are compact and energy-efficient, making them ideal for specialty oil producers.
For medium to large capacities, the HPDF 550 or HPDF 700 are the gold standards. With the HPDF 700 capable of processing up to 30,000 L/H (in specific configurations), it is designed for the most demanding industrial environments. These models prioritize throughput and stability, utilizing higher power motors to maintain high G-forces during separation.
Below is a detailed breakdown of the technical parameters for the most popular models, providing a clear comparison of capacity, power, and physical dimensions to assist in your selection process.
Technical Comparison of Centrifuge Separator Models
| Model |
Capacity (L/H) |
Power (KW) |
Weight (KG) |
| DHZ 360 |
1200-2500 |
7.5 |
1280 |
| DHZ 550A |
5000-10000 |
18.5 |
2200 |
| HPDF 400E |
4000-7500 |
7.5 |
1300 |
| HPDF 550 |
6000-18000 |
22 |
2200 |
| HPDF 700 |
15000-30000 |
30 |
3300 |
| HPDF 360 |
1200-2500 |
5.5 |
750 |
FAQS
Our separators are designed for a wide range of vegetable oils, including rapeseed, cottonseed, corn, palm, soybean, peanut, sunflower, rice bran, sesame, and safflower oil. The personalized solutions provided by the DHZ and HPDF series allow for the optimization of the separation process based on the specific viscosity and impurity levels of each oil type.
The PLC (Programmable Logic Controller) automates the residue-extraction of the slide piston. This means the machine can automatically discharge solids without stopping the flow, making it highly adaptive to changes in crude oil quality. This reduces the need for constant manual monitoring and minimizes labor costs while maintaining peak efficiency.
Yes, the equipment is highly effective for animal oil purification, including fish oil and fat purification from various other animals. Because all contacting parts are made of stainless steel, it prevents chemical reactions and contamination, ensuring the purified animal fats meet high health and safety standards.
The hydraulic coupler, paired with helical step-up gears, allows for a liquid-based power transmission. This ensures that the machine accelerates steadily and provides essential overload protection. This reduces the mechanical stress on the motor and gears, leading to a longer lifespan and more stable operation under heavy loads.
Absolutely. While optimized for oil, these separators are applicable for separating any suspension liquid—including two liquids or a liquid and solid—that have different specific gravities. This makes them a versatile choice for the light industry, chemical, medicine, and food sectors.
The top-fed design allows the machine to operate with very low inlet pressure. This is a significant advantage for refinery plant managers as it simplifies the feed pump requirements and reduces the energy needed to move the material into the separator, contributing to overall operational cost savings.
Conclusion
The implementation of a high-efficiency centrifuge separator is a transformative step for any edible oil or industrial refining plant. By combining stainless steel construction, PLC-driven automation, and a sophisticated hydraulic drive system, these machines maximize production capacity while ensuring the highest purity of the final product. Whether processing vegetable oils or animal fats, the ability to continuously degum, desoap, and wash materials makes this technology indispensable for modern industrial standards.
As the industry moves toward greater automation and sustainability, investing in scalable and durable separation technology is key to maintaining a competitive edge. We recommend selecting a model based on specific capacity needs to optimize energy consumption and yield. To explore the full range of our oil processing solutions, visit our website: www.oilmillchina.com